What Spray Transfer Provides on Carbon Steel: A Shop-Floor Guide
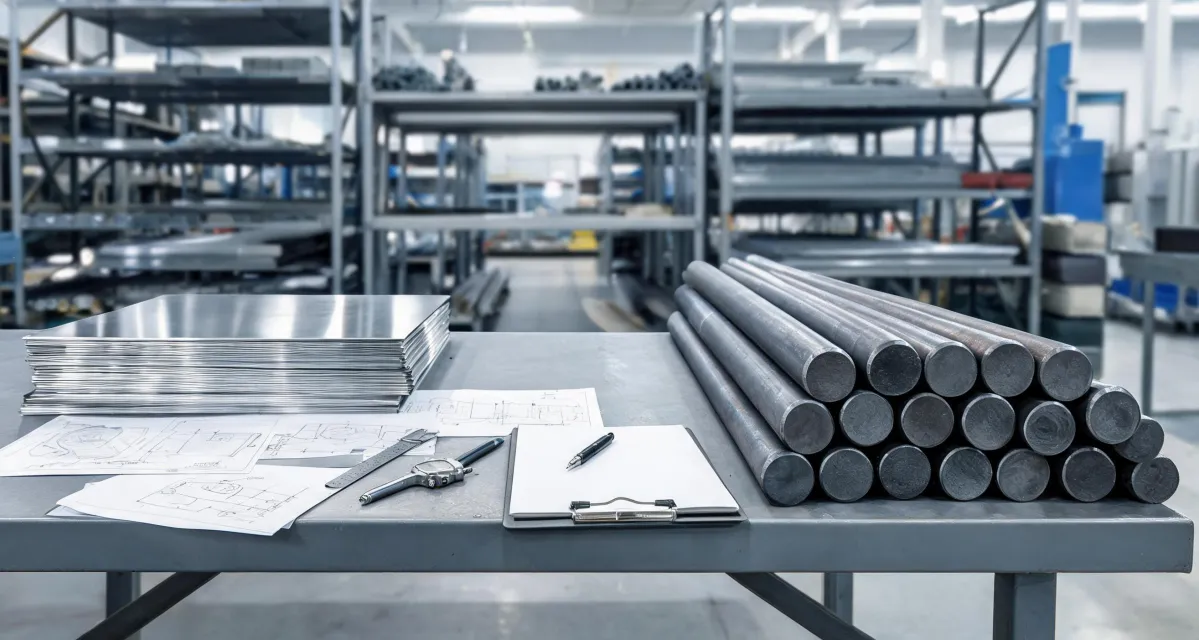
In nearly every fabrication shop, there is that job: a rack of carbon steel brackets, each one a half-inch thick, needing a full fillet weld on both sides. The operator reaches for short-circuit transfer because it is what he learned, what the machine was set up for, and what will run without complaint on the thinnest sheet in the building. The gun weaves to compensate, the wire sputters, and a fine mist of sparks coats the table, the clamps, and the front of the hood. Each pass leaves a bead that looks passable in dim shop light, but the penetration is shallow, the profile is ropey, and the grinder runs for ten minutes after every joint to knock down the spatter that has frozen into the corners. The parts go out, the next batch comes in, and the same cycle repeats because nobody stops to ask why the process itself is causing the cleanup. The answer is that short-circuit transfer is a low-energy mode, and low energy cannot drive a weld deep into thick carbon steel.
A Messy Start on the Bench
Every fabrication shop has that job: a rack of carbon steel brackets, each one a half-inch thick, needing a full fillet weld on both sides. The operator reaches for short-circuit transfer because it is what he learned, what the machine was set up for, and what will run without complaint on the thinnest sheet in the building. The gun weaves to compensate, the wire sputters, and a fine mist of sparks coats the table, the clamps, and the front of the hood. Each pass leaves a bead that looks passable in dim shop light, but the penetration is shallow, the profile is ropey, and the grinder runs for ten minutes after every joint to knock down the spatter that has frozen into the corners. The parts go out, the next batch comes in, and the same cycle repeats because nobody stops to ask why the process itself is causing the cleanup. The answer is that short-circuit transfer is a low-energy mode, and low energy cannot drive a weld deep into thick carbon steel.
What would change if the same operator switched to spray transfer? The question sounds theoretical until you price the wasted consumables and the extra labor. Spray transfer needs an argon-rich gas mix and a current setting above a threshold, which many shops never try because they assume the machine is not capable or the steel is not suitable. But carbon steel is, in fact, one of the best candidates for the process, and the reason has everything to do with physics rather than brand loyalty. The practical question is not whether spray transfer can run on carbon steel, but how it changes the economics of a flat-position job, and under what conditions the trade-offs stop making sense. This article walks through the mechanism, the payoffs, and the limits, so the next rack of brackets can go out with less spatter, deeper penetration, and a finish that does not need a grinder.
See What Changes Inside the Arc
Spray transfer is a mode of metal transfer in which the molten wire crosses the arc as a stream of tiny droplets, driven by a high current and the pinch effect of the magnetic field. The droplets are smaller than the wire diameter, they move at high speed, and the arc is steady rather than erratic. A useful comparison comes from advanced manufacturing: in a 2020 study of nickel-aluminum-bronze parts made by wire arc additive manufacturing, researchers used cold metal transfer (CMT) to control heat input and bead shape, because that alloy would not tolerate the heat of a conventional spray arc. The contrast is revealing—aluminum bronze needs a gentle, controlled pulse, while carbon steel, with its higher thermal conductivity and stable oxide behavior, accepts the hotter, more energetic spray stream without the same risk of warping or porosity. That one difference explains why spray transfer, which is almost a problem for aluminum alloys, becomes an asset on carbon steel.
The physical mechanism starts with current density. When the welding current rises above the transition current for a given wire diameter, the electromagnetic force pinches the molten tip until it detaches into a spray of fine drops instead of one large short-circuiting bridge. This pinch effect depends on the shielding gas: a blend of at least 80% argon with up to 20% CO2 creates the constricted arc needed for stable spray, while pure CO2 or a low-argon mix cannot support the transfer and falls back into globular or short-circuit modes. The current threshold itself is not a fixed number, but for a common 0.045-inch solid wire on carbon steel it sits around 200 amperes, a range that most shop machines can reach. At that point, the arc voltage rises, the arc column becomes cone-shaped, and the cathode jet pushes the droplets straight into the weld pool. Each droplet arrives with enough energy to stir the pool and melt the base metal ahead of the arc, which is why the weld root gets the same fill as the cap. This is a cause-and-effect chain: high current begets fine droplets, fine droplets beget a narrow arc, and a narrow arc begets deep, consistent fusion.
The contrast with aluminum is the clearest way to see why carbon steel takes to spray transfer. Aluminum is about one-third the density of steel, conducts heat and electricity roughly 62% as well as copper by cross-section, and forms a tenacious oxide layer that vaporizes at a higher temperature than the base metal. Those properties are the reason aluminum welding relies on alternating current, oxide-cleaning action, and a strict heat budget—the same energy that would build a clean spray arc on steel can burn through an aluminum joint or leave it with a messy oxide inclusion. The Alro Steel technical manual notes these very behaviors: aluminum's light weight and corrosion resistance make it ideal for many applications, but its process demands differ from steel's. For a fabricator working in carbon steel, that means the process that gives you trouble on aluminum—a hot, concentrated spray arc—is exactly what the steel has been waiting for. The material does not fight the high current; it conducts it quickly and lets the molten drops flow into a deep, clean puddle.
Watch Your Production Numbers Move
The first payoff shows up in deposition rate. A spray transfer weld at 250 amperes puts down several times more metal per minute than a short-circuit weld at the same heat input, because every drop carries a larger volume and the wire feed speed climbs with the current. On a flat fillet weld, this translates into fewer passes; a joint that needed three beads with short-circuit might need one or two with spray. The arithmetic works in the shop: less time under the hood, less consumable per joint, and a lower cost per foot of weld. The cause is again the physics—the high-current spray releases energy continuously rather than in the pulses of short-circuit, so the wire melts faster and deposits at a rate that approaches the machine's top feed speed. For a shop that runs repetitive carbon steel assemblies, the difference is not a few seconds but a measurable increase in daily output.
Penetration is the second payoff, the property that most directly affects whether a weld holds. Spray transfer drives the arc deep into the base metal, creating a finger-like fusion profile that reaches the root of a heavy joint without requiring a bevel or a root pass. Deep penetration means the weld cross-section is larger and stronger than what short-circuit can produce at the same amperage, and it reduces the risk of lack-of-fusion defects in thick sections. On a half-inch carbon steel plate, a spray weld at 260 amperes can fully fuse the joint in a single pass where short-circuit would leave a cold lap at the root. The penalty of the added heat is real—it can cause distortion on thin material—but for material above a quarter-inch, the penetration benefit outweighs the heat input. That is why structural welders choose spray when the position allows.
The cosmetic payoff, the third, is anything but trivial: spray transfer produces little or no spatter, so the weld surface is smooth, clean, and often ready for paint without grinding. The reason is that the metal transfers as droplets that land in the puddle without bridging the gap and shorting, which is the event that creates spatter in short-circuit welding. The surface finish also benefits from the stable arc, which leaves a uniform ripple and a flat profile. The comparison to aluminum temper is useful here: just as a 3003-H14 sheet behaves differently from a 6061-T6 because the temper changes the material's response to forming, the same wire and gas can produce very different weld finish depending on the transfer mode selected. The process parameters are the 'temper' of the weld—set them correctly, and the cosmetic and mechanical properties follow.
Draw the Line at Flat and Thick
Spray transfer is not a universal answer, and the limits are as important as the benefits. The process works only when the weld is flat or horizontal; in vertical or overhead positions, the large molten puddle and high heat input will run or sag out of the joint. The current must stay above the transition threshold for the wire size, which typically means a minimum of 180–220 amperes for 0.045-inch wire, and the shielding gas must be argon-rich, usually 75–90% argon with the balance CO2 or oxygen. If the gas mix drops below that range, the transfer falls into globular mode, which produces heavy spatter and poor penetration, effectively losing all the advantages. The current must also be matched to the material thickness: a 1/16-inch sheet will simply burn through at spray currents, so the process is reserved for material roughly 3/16-inch and thicker.
The material's own properties set the boundary. When a supplier helps a customer choose between 3003, 5052, and 6061 aluminum, the decision depends on strength, corrosion resistance, and formability—the alloy's response to the fabrication process. The same logic applies to welding: carbon steel's thermal conductivity and oxide behavior make it a natural fit for spray transfer, but only within a thickness and position window. On thin sheet, the high heat input causes distortion and burn-through, so short-circuit or pulse modes are the right call. In vertical and overhead work, gravity overpowers the surface tension of the spray puddle, so the process cannot hold the weld. The decision rule is therefore not 'spray is better' but 'spray is better when the joint is thick enough to accept the heat and positioned so the puddle can stay in place.' That is the non-obvious judgment that separates a competent fabricator from one who blindly cranks up the amperage.
A Rule You Can Carry to the Next Job
Back on that fabrication bench, the same rack of brackets is set up with a new gas bottle and a bump in the voltage. The operator hits the trigger, and the arc settles into a steady hum instead of a staccato sputter. The wire leaves a shower of fine droplets that disappear into the puddle, the spatter that used to decorate the table is nearly absent, and the first bead comes out flat and clean. He runs the second side, then checks the back of the joint—the penetration line is visible all the way through, something the short-circuit passes never showed. The grinder stays in the drawer, and the parts move to the paint line with no rework.
The rule from the shop floor is short enough to remember: spray transfer on carbon steel when the joint is flat or horizontal and the material is thick enough to absorb the heat. For anything thinner than about 3/16-inch, for vertical or overhead work, or for a gas bottle that is not argon-rich, short-circuit or pulse remain the right tools. The mechanism is not magic—it is the predictable result of high current, argon-rich gas, and a material that conducts heat without fighting back. Once a welder understands that cause-and-effect chain, the choice stops being a rumor and becomes a calculation: when the conditions are right, spray transfer pays in speed, penetration, and cleanup; when they are not, it punishes the work with burn-through and dripping puddles. That is the whole guide, and it fits on a sticky note above the bench.
The rule from the shop floor is short enough to remember: use spray transfer on carbon steel when the joint is flat or horizontal and the material is thick enough to absorb the heat. For anything thinner than about 3/16-inch, for vertical or overhead work, or for a gas bottle that is not argon-rich, short-circuit or pulse remain the right tools. The mechanism is no magic—it is the predictable result of high current, argon-rich gas, and a material that conducts heat without fighting back. Once a welder understands that cause-and-effect chain, the choice stops being a rumor and becomes a calculation: when the conditions are right, spray transfer pays in speed, penetration, and cleanup; when they are not, it punishes the work with burn-through and dripping puddles. That is the entire guide, and it fits on a sticky note above the bench.
Ingrid Solberg
Ingrid Solberg is an independent carbon and structural steel analyst covering steel plate, sheet, coil, pipe, beams, rebar, and galvanized products. She applies ASTM A36/A36M and A6/A6M requirements while comparing grade chemistry, yield strength, tensile strength, elongation, dimensional tolerance, weldability, and surface condition. Her evidence-led guides help engineers, fabricators, and procurement teams select suitable steel forms, define purchase specifications, and evaluate mill or service-center offers.