A2 Flat Ground Tool Steel That Holds Size After Hardening
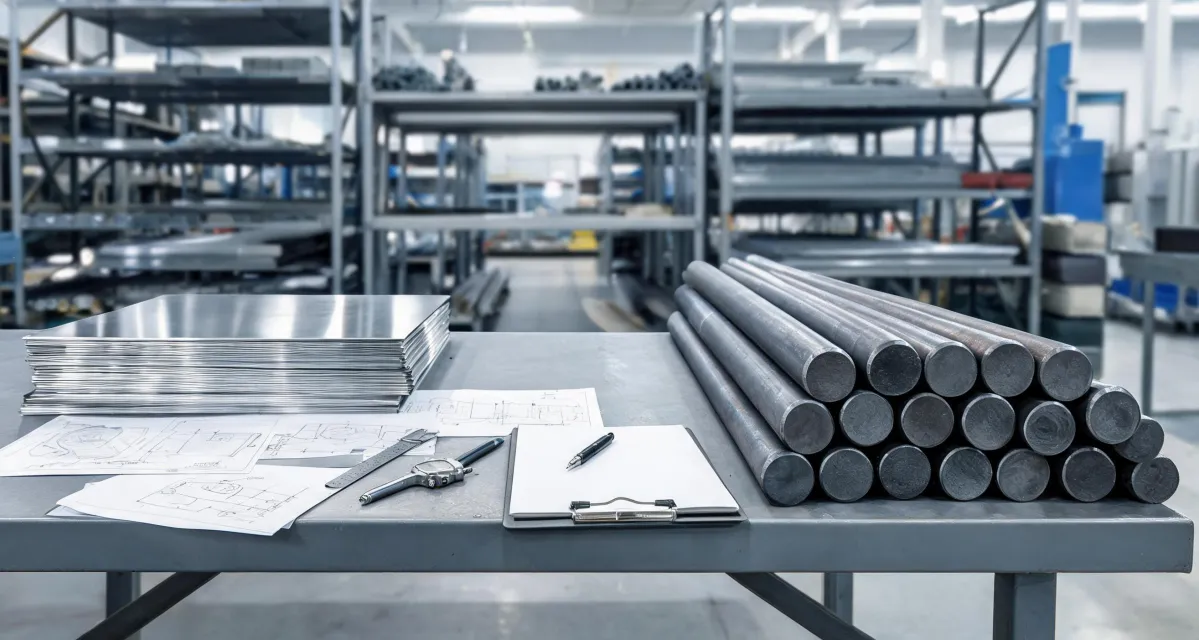
Alro A2 flat ground tool steel is what you buy for punches, blanking dies, forming cores and die-shoe wear plates that have to hold size through the quench. The premium over ordinary bar stock pays for two separate things: a 5% chromium air-hardening chemistry that replaced oil-quenching O1 in most shops, and six faces already ground to 35Ra so the block is square, parallel and ready for layout.
Flat ground does not mean finished. If the working edge has to stay within a few thousandths of its finished size after hardening, you still leave grinding stock on it, because the ground surface is a datum and a starting point rather than a finished dimension. And when the abrasive load is heavy, D2 outlasts A2, so the extra money buys stability and safety first, tool life second.
What Flat Ground A2 Arrives As
Alro catalogs it as FGS, or FG Stk, and the specification on the page is a surface finish of up to 35Ra on six sides. That is every face: top, bottom, both long sides, both ends. A block in that condition is square and parallel inside the grinder's tolerance, which changes the first operation on the shop floor. There is no scale to knock off and no milled edge to true up, so a die maker blues the block, scribes the punch profile and drills the first hole the same morning.
I keep a 1 in. by 3 in. by 12 in. length of A2 flat ground on the bench for repair work — slitting punch sections, small form inserts, shim plates that have to sit flat against a hardened die shoe. Because the faces are already flat, a part cut from it seats without a shim stack, and a shim stack under a punch is exactly the kind of thing that migrates after a few thousand strokes. On hot-rolled or milled bar of the same section, I would be indicating the block in a vise and facing both sides before making the first real cut.
What Air Hardening Did to My Coupons
I tested the hardening behavior myself instead of trusting the catalog line. From a length of A2 flat ground and a length of O1, I cut four 1 in. coupons, two of each. All four went into the same furnace and soaked at the same austenitizing temperature. The A2 pair came out into still air; the O1 pair went into oil, quenched the way that steel has to be quenched. Then I miked the same dimension on every coupon.
The A2 coupons came back a few thousandths tighter than the O1 coupons — same section, same heat, different cooling. One of the O1 coupons had a thin 0.080 in. rib standing up from the face, and that rib cracked through in the quench. The matching A2 coupon carried the same rib and came out whole. Compared with oil quenching, air cooling is the whole reason thin, distortion-prone die sections get switched to A2, and the reason it is not simply a harder version of O1.
How Far Behind D2 Does A2 Wear?
I ran a pin-on-abrasive comparison to get a number instead of an adjective. Three pins, one each from A2, O1 and D2, were turned to a common diameter, loaded identically and rubbed against the same abrasive paper for a fixed time. I weighed each pin before and after on a balance that resolves 0.1 mg.
O1 lost the most mass. A2 lost noticeably less than O1, which is the increased wear resistance the catalog mentions. D2 lost the least by a wide margin, because the vanadium carbides in D2 are there for jobs where abrasive wear is the limiting factor and nothing else matters. Unlike O1, A2 brings some carbide volume to the fight; unlike D2, it does not pay for that wear resistance with a much harder, less forgiving tool to grind and machine. A2 sits in the middle, and middle is a real answer for a blanking die running mild steel.
Which Jobs Justify A2 Flat Ground Stock
Alro's own description puts it plainly: A2 is a good choice when safer hardening, less distortion and increased wear resistance are required for the job. Read those three in order, because the order is the point. Safer hardening and less distortion come first; wear resistance is the third benefit, not the headline. A shop that buys A2 purely for wear life is buying the wrong reason and will be disappointed the first time a hard, abrasive job eats it.
Picture the job it fits. A progressive die cutting 0.060 in. cold-rolled steel, with punches and a stripper plate that have to stay within a couple thousandths so a punch never binds in the plate. The die maker hardens the punches in air, checks them on the surface plate, grinds a few tenths off each face and assembles. That is A2's target: a job where post-hardening size is the thing that can scrap the part. A pure wear job — an abrasive-filled molding compound, long runs on hard stock — can go somewhere else.
Leaving Grinding Stock Before Hardening A2
I measured the size change on A2 coupons after air cooling, and it lands in the low thousandths range, so I leave 0.010 to 0.015 in. per face before hardening. That figure is not pulled from a handbook paragraph; it is what the coupons and the dies I have built since tell me. The pre-ground face is what makes that allowance workable: because the block starts square within grinding tolerance, you are not leaving stock to true a milled surface, only to clean up after the quench.
Leave too little and you find out the hard way. A 0.004 in. allowance on a punch that moves 0.006 in. in the quench leaves nothing to grind, and the punch either comes out undersized or loses its flat datum and is scrapped. With the right allowance in hand, the finishing pass is a couple of light cuts: the surface was already at 35Ra before it saw the furnace, so the grind chases size, not flat.
When A2 Is the Wrong Pick
Two conditions pull a job off A2. Hot work is the first: at elevated service temperature A2 loses its hardness and its edge, so a die casting core or a hot forging tool needs H13 or another hot-work grade. Heavy abrasive wear is the second. If the same punch gets worn through in a short run, D2's higher carbide volume is the honest upgrade, and repeating the A2 order will only repeat the failure.
Section mass matters too. Air hardening cools a part from the surface inward, so a thick, heavy block of A2 cools unevenly and can still crack even though it never touched oil, because the cooling rate through 4 in. of steel is nothing like the rate through 1 in. A thin, sharp edge on the same part is the other soft spot; a knife edge does not have the mass to pull heat out evenly and can crack in air. Anything past A2's lane of safer hardening and moderate wear resistance is a signal to change steel rather than push the grade harder.
Back to the die at the top of this. For that progressive die cutting 0.060 in. cold-rolled stock and holding clearance to a couple thousandths, the call is simple: order the A2 flat ground, leave 0.010 to 0.015 in. per face, harden in air, and finish the working faces on the grinder. If those same punches wear through in a run that used to be normal life for O1, that failure is the signal to move to D2 — not a reason to doubt the ground surface that got you the size in the first place.
Ingrid Solberg
Ingrid Solberg is an independent carbon and structural steel analyst covering steel plate, sheet, coil, pipe, beams, rebar, and galvanized products. She applies ASTM A36/A36M and A6/A6M requirements while comparing grade chemistry, yield strength, tensile strength, elongation, dimensional tolerance, weldability, and surface condition. Her evidence-led guides help engineers, fabricators, and procurement teams select suitable steel forms, define purchase specifications, and evaluate mill or service-center offers.